QT5-15 Automatic Concrete Block Molding Machine
Hydraulic pressure plus high frequency vibration forming blocks in 15 to 20 seconds.
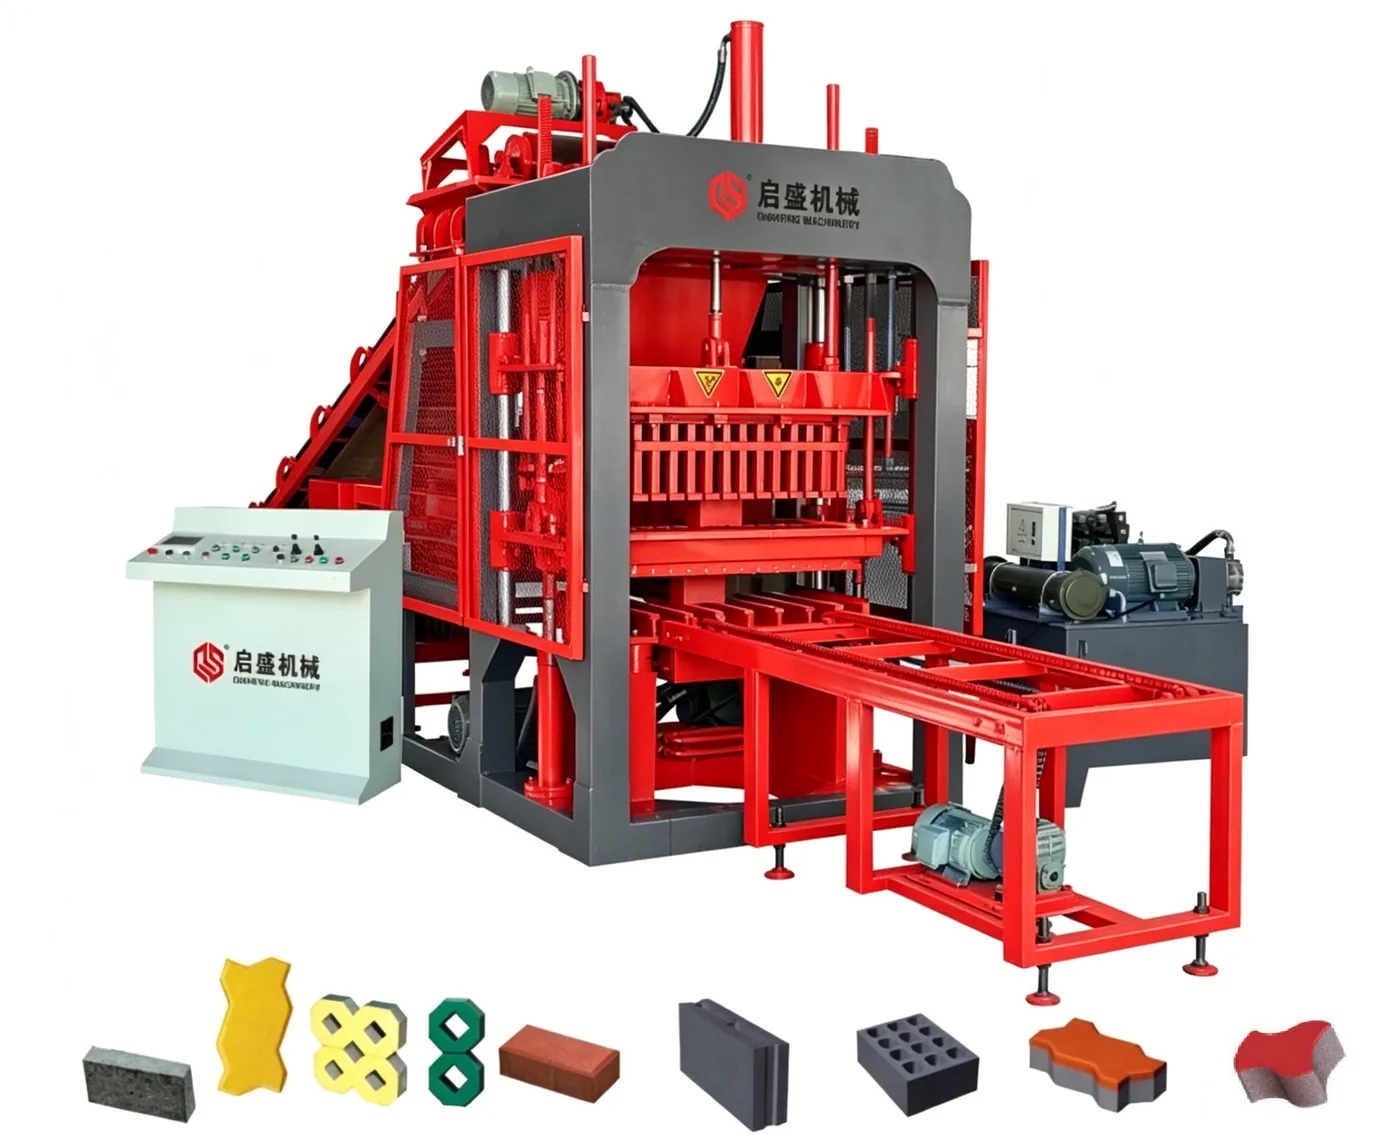
The QT5-15 is a fully automatic block molding machine for medium and large building materials plants. It forms blocks by combining high frequency vibration with hydraulic pressure, so material packs quickly and evenly into the mould and the finished unit leaves with dense structure, even corners and tight dimensional tolerance. A forming cycle of 15 to 20 seconds sets the working rhythm, and a 58 kN excitation force with 25 MPa forming pressure does the compaction. Total installed power is 37.4 kW, with a separate 2.25 kW feeding motor. A PLC and industrial touch screen run the whole sequence, from feeding and forced distribution through vibration and pressing to demoulding, brick removal and pallet return. One touch sets parameters, the screen shows live status, and faults are reported with a diagnosis rather than a bare code. The host frame is welded as one piece and stress relieved by aging, which is what allows it to hold accuracy under continuous high frequency vibration. Batching machines, mixers, belt conveyors and automatic stackers connect directly to build a complete line. Moulds can be changed between block types inside a shift, so one machine serves hollow blocks, pavers and solid units.
Configured around output, blocks and operating conditions.
High frequency vibration combined with 25 MPa hydraulic pressure forms dense blocks in one stroke., Forming cycle of 15 to 20 seconds with 58 kN excitation force from the vibration system., Total installed power of 37.4 kW, including a dedicated 2.25 kW feeding motor., Heavy integral welded frame, stress relieved by aging, resists long term vibration without distortion., PLC with industrial touch screen runs feeding, distribution, pressing, demoulding and pallet return., Pallet size of 1,100 x 650 x 20 mm and host weight of 6,900 kg for stable pressing.
Typical decision factors
What changes the machine price?
Daily capacity
Output target determines machine size, mould cycles and line configuration.
Automation
Pallet handling, cubing, batching and packaging change total project scope.
Block types
Hollow block, paver, interlock and curbstone may require different moulds and handling.
Service scope
Shipping, installation, training and spare parts are quoted by destination.
Composite Forming in a 15 to 20 Second Cycle
The QT5-15 molds blocks by combining high frequency vibration with hydraulic pressure. Vibration fluidises the mix so it flows into every corner of the mould, then the hydraulic unit applies a forming pressure of 25 MPa to lock the structure before demoulding. The two actions run as one stroke rather than as separate stages, and a forming cycle of 15 to 20 seconds sets the production rhythm of the line.
Blocks leave with even edges, stable strength and dimensional tolerance held tighter than the usual site requirement. Pallet size is fixed at 1,100 x 650 x 20 mm, so pallet handling equipment can be specified once and kept for the life of the line.
Drive, Power and Frame Construction
Total installed power is 37.4 kW, of which a dedicated 2.25 kW motor drives the feeding and distribution box. An excitation force of 58 kN is delivered into the mould, which is high enough to handle stiff, low slump mixes that older vibration-only machines struggle with.
The host is built around a heavy integral welded frame, stress relieved by aging treatment before machining. That matters more than it sounds: continuous high frequency vibration and pressing will distort a frame that was only bolted together, and once the frame moves, block height tolerance moves with it. Host weight is 6,900 kg and the host envelope is 9,450 x 3,300 x 2,700 mm.
PLC Sequence and Operator Control
A PLC programmable controller and an industrial touch screen handle the full sequence: raw material feeding, forced material distribution, vibration and pressing, demoulding and brick removal, then pallet recycling. Each step is coordinated with the next, so the machine keeps a steady cycle without an operator standing at the mould.
Parameters are entered once and stored as recipes. The screen shows live machine status, and the diagnostic function names the step that failed instead of showing only a fault number. For a plant running several block types per shift, that shortens the changeover between moulds.
Building a Complete Block Line
The QT5-15 connects directly with batching machines, mixers, belt conveyors and automatic stacking machines. A line assembled from these modules moves material without manual handling between stations, which cuts both labour cost and the physical workload on the crew.
Typical buyers are municipal building materials producers and solid waste resource recovery plants making non-fired units. Before sizing the line, agree on the pallet count and the curing area, because stacking capacity rather than moulding speed is usually what limits daily output.