QST1200 Concrete Mixing Plant for Ready-Mix Supply
Twin-shaft forced mixing and PLC control for steady, high-volume concrete output.
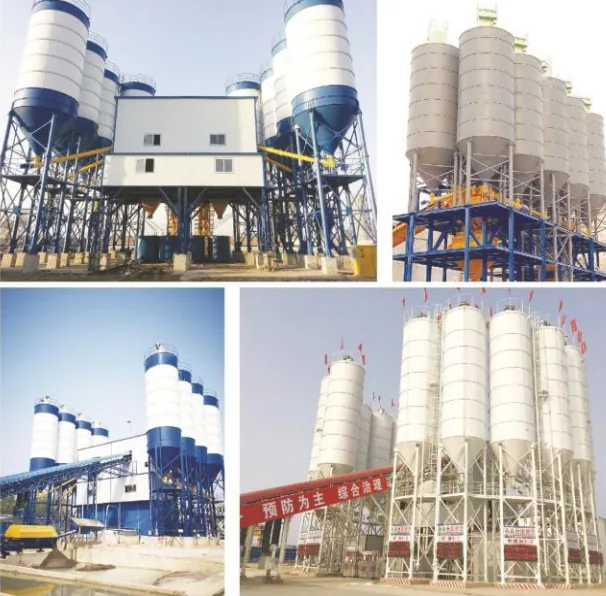
The QST1200 is a stationary concrete mixing plant built for ready-mix suppliers and large civil works where batching accuracy and continuity of output decide the project schedule. A twin horizontal shaft forced action mixer does the central work, blending aggregate, cement, water and admixtures in a short cycle so each batch leaves the drum at a similar density and strength. The plant handles dry-hard, semi-dry-hard and plastic mixes without changing internals. Metering, feeding, mixing and discharge run through a networked automatic control system with a PLC and an industrial touch screen, so a recipe is set once and the cycle is followed on screen. Mixing blades cast in high chromium manganese alloy resist abrasion from crushed stone, and the shaft ends use a multi seal arrangement that keeps slurry out and lubricant in. Combined, the wear resistant internals and sealed shafts hold unplanned downtime low on sites running two or three shifts a day. Discharge feeds mixer trucks directly, and walkways are laid out for quick inspection and blade replacement. Two frame levels keep the aggregate handling area apart from the cement and admixture lines, so fine material does not contaminate the coarse bins.
Configured around output, blocks and operating conditions.
Twin horizontal shaft forced action mixer blends dry-hard, semi-dry-hard and plastic mixes uniformly., PLC with industrial touch screen runs weighing, feeding, mixing and discharge as one automatic sequence., Mixing blades cast in high chromium manganese alloy resist impact and abrasion from crushed stone., Multi seal shaft ends stop slurry leakage and dust entry, reducing unplanned mixer downtime., Batch data logging and networked monitoring give traceable records for every delivered load.
Typical decision factors
What changes the machine price?
Daily capacity
Output target determines machine size, mould cycles and line configuration.
Automation
Pallet handling, cubing, batching and packaging change total project scope.
Block types
Hollow block, paver, interlock and curbstone may require different moulds and handling.
Service scope
Shipping, installation, training and spare parts are quoted by destination.
Stationary Output for Daily Pour Schedules
The QST1200 concrete mixing plant is configured for sites that pour every working day: ready-mix depots, civil contractors and industrial builders who cannot wait on batches. Material flow from the aggregate bins through the mixer to the discharge point is arranged so that charging, mixing and emptying overlap instead of running one after the other. That overlap is what keeps hourly throughput steady when a project switches from one concrete grade to the next inside the same shift.
Because the unit is stationary, frames, bins and walkways are sized for long service rather than transport. Operators reach the mixer platform, the cement screw and the water and admixture lines from one deck, which shortens the daily inspection walk and keeps the working area clear.
Twin-Shaft Forced Mixing and Batch Consistency
At the centre of the plant sits a twin horizontal shaft forced action mixer. Two counter-rotating shafts pull the charge in opposite directions, so aggregate, cement, water and admixtures meet in a fast rolling motion rather than a slow tumble. This is why the same machine covers dry-hard, semi-dry-hard and plastic mixes without internal changes, and why segregation at the end of the mix is rarely a problem.
Metering runs on separate channels for aggregate, cement, water and admixture. Correct proportioning at the gate is the cheapest way to protect strength, because extra mixing time cannot rescue a batch that was weighed wrong in the first place.
PLC Control, Monitoring and Batch Records
The control package combines a PLC, an industrial touch screen and networked monitoring. Recipes are stored as numbers, not as operator memory, so a change of shift does not change the mix. The screen follows the sequence live through weighing, feeding, mixing and discharge, and alarms point to the step that stopped rather than reporting a bare fault code.
Batch data can be logged and reviewed remotely, which matters when a client asks for proof of what was delivered. Traceable records also expose a slow drift in aggregate moisture or cement flow before it turns into a rejected load.
Wear Parts Chosen for Abrasive Aggregate
Mixing blades are cast in high chromium manganese alloy, selected for impact and abrasion resistance when crushed stone and gravel pass through the drum week after week. Shaft ends use a multi seal arrangement that separates the bearing housings from the wet side of the mixer, keeping slurry out and lubricant in.
Those two details decide how often the mixer is opened for repair. Plants running two or three shifts feel it most, because a leaking shaft seal stops production at the worst possible time. Blade clearance can be adjusted, so a worn set returns to tolerance before it is replaced.