QST1200 Foamed Concrete Block Production Line
Non-autoclaved foamed blocks from fly ash, tailings and slag at lower investment.
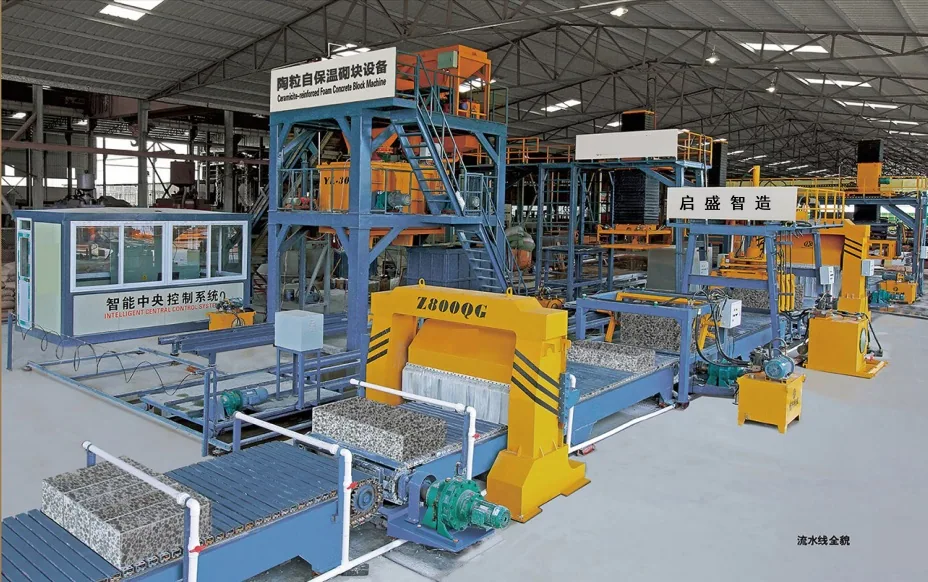
The QST1200 foamed concrete block line makes lightweight wall blocks through a non-autoclaved process, so the high pressure steam curing vessel and its fuel bill are removed from the works. Raw material comes from industrial by-products such as fly ash, tailings, industrial slag and stone powder, which are usually available locally and cheap, so material cost falls while solid waste is reused. Investment in the line is about 40 to 50 percent of a traditional autoclaved aerated concrete plant of similar role, and the compact equipment layout lowers the entry barrier for smaller building materials producers. A composite additive developed in house creates a closed-cell structure inside the block, which cuts water absorption and improves freeze-thaw resistance and thermal insulation. Strength and insulation are therefore held together rather than traded off. Automation covers proportioning, mixing, foaming, mould filling and demoulding, keeping the cycle repeatable from one shift to the next. Blocks are demoulded and stacked to cure, and the line accepts several ash sources so production does not depend on a single supplier.
Configured around output, blocks and operating conditions.
Runs on fly ash, tailings, industrial slag and stone powder as primary raw material inputs., Non-autoclaved process removes the high pressure curing vessel and its fuel consumption., Investment of about 40 to 50 percent of a traditional autoclaved aerated concrete line., Composite additive creates closed cells that lower water absorption and raise freeze-thaw resistance., Foamed blocks combine load-bearing strength with thermal insulation in one wall unit., Automatic proportioning, foaming, mixing, mould filling and demoulding keep the cycle repeatable.
Typical decision factors
What changes the machine price?
Daily capacity
Output target determines machine size, mould cycles and line configuration.
Automation
Pallet handling, cubing, batching and packaging change total project scope.
Block types
Hollow block, paver, interlock and curbstone may require different moulds and handling.
Service scope
Shipping, installation, training and spare parts are quoted by destination.
A Line Built Around Industrial By-Products
The QST1200 foamed block line is designed to run on material that plants already have nearby: fly ash, tailings, industrial slag and stone powder. These by-products are cheap, widely available and otherwise a disposal problem, so a block plant using them lowers its raw material cost and its waste footprint at the same time.
Because the recipe accepts a range of sources, the line is less exposed to a single supplier. Where a plant changes its ash source, the foaming agent dose and mixing time are the two settings that need rechecking first.
Non-Autoclaved Curing and Lower Investment
Curing is done without a high pressure autoclave. Removing that vessel takes the steam boiler, the pressure vessel inspection and a large share of the fuel cost out of the project. Investment in the line settles at roughly 40 to 50 percent of a traditional autoclaved aerated concrete plant of comparable role, and the equipment footprint is compact enough for a small building materials enterprise to adopt.
What replaces the autoclave is a controlled foaming and curing sequence. The mix is foamed to a target density, poured, left to set, and then demoulded and stacked to cure. Each of those steps has to be repeatable, otherwise block weight and insulation drift from batch to batch.
Closed-Cell Structure and Block Performance
A composite additive developed in house generates an independent closed-cell structure inside the block. Closed cells are the reason a lightweight foamed unit can hold strength while still insulating, because they block water and reduce the paths along which heat travels. The practical results are lower water absorption and clearly better freeze-thaw resistance and thermal conductivity.
That combination meets building energy efficiency design requirements without adding a separate insulation layer to the wall, which is often the deciding factor when a project compares foamed block masonry against conventional brickwork.
Automation and Production Discipline
Proportioning, foaming, mixing, mould filling and demoulding run under automatic control. Automation matters more here than in fired brick production, because foamed density is sensitive to the accuracy of the additive dose and to the time between foaming and pouring. Manual variation shows up later as rejected blocks.
The process also avoids high pressure steam, which keeps the working environment simpler and reduces the amount of specialist maintenance a small plant has to carry.
Before ordering, agree on the stacking and curing area, because those two decide daily output far more than the nominal cycle time does.