Cement Block Making Machine
Cement-sand-aggregate block production with configurable automation.
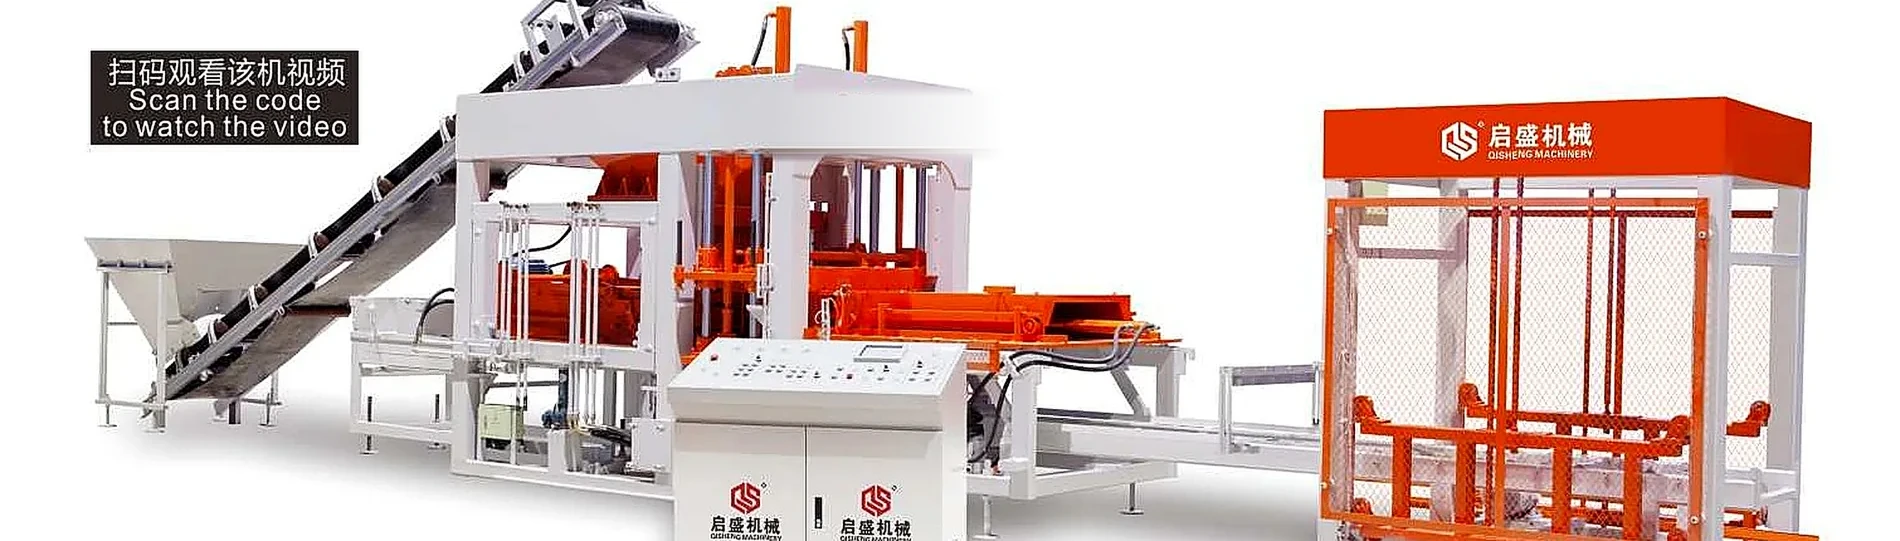
Cement block making machines from the QST8-15 and QST6-15 range form solid bricks, hollow blocks and pavers by vibration and hydraulic press moulding. This page covers what each model can produce, real capacity and power figures, the moulds and raw materials involved, the factors that decide the price, and the installation, training and spare part support offered to buyers in Syria and across the Middle East.
Configured around output, blocks and operating conditions.
PLC control, hydraulic forming, replaceable moulds, configurable automation, installation and training support.
Typical decision factors
What changes the machine price?
Daily capacity
Output target determines machine size, mould cycles and line configuration.
Automation
Pallet handling, cubing, batching and packaging change total project scope.
Block types
Hollow block, paver, interlock and curbstone may require different moulds and handling.
Service scope
Shipping, installation, training and spare parts are quoted by destination.
What a Cement Block Making Machine Can Produce
A cement block making machine is chosen by the product you sell, not by the model number. One QST8-15 or QST6-15 host does the work, and the finished block changes with the mould. Solid bricks, hollow load-bearing blocks, partition blocks, cement pavers and interlocking blocks all come off the same machine once the mould is set for that shape and the mix is adjusted to suit it.
Most buyers in the region start with hollow blocks for wall construction and add pavers as the order book grows. If your market buys two block sizes in the same week, plan the mould changes and the daily running order before you fix the machine. A second mould costs far less than a second machine, and the changeover on this platform is a mechanical swap, not a rebuild.
- Standard solid bricks and paving bricks
- Hollow load-bearing blocks and partition blocks
- Cement pavers, interlocking blocks and lawn pavers (mould dependent)
- Kerb stones and shaped concrete products (mould dependent)
- Thin products only where the mould and the mix are specified for them
Tell the supplier which block is the first product you will sell and which is the second. The mould set and the pallet size follow from that answer, and settling it at order time avoids a second shipping round later.
Models and Configuration: QST8-15 and QST6-15
Two models cover this page. Both use imported hydraulic proportional components, an intelligent PLC touch screen, arch-breaking rapid distribution for an even fill, and extended high-efficiency vibration. The difference is size, pressure and output, so the choice comes down to transformer capacity, building size and target pieces.
| Parameter | QST8-15 | QST6-15 |
|---|---|---|
| Machine size | 9,800 × 3,600 × 2,800 mm | 9,450 × 3,300 × 2,700 mm |
| Pallet size | 980 × 860 × 22 mm | 980 × 680 × 20 mm |
| Vibration frequency | 3,800 to 4,500 times / min | 3,800 to 4,500 times / min |
| Vibration force | 95 kN | 68 kN |
| Rated pressure | 31.5 MPa | 25 MPa |
| Installed capacity | 44.9 kW | 34.4 kW |
| Moulding cycle | 15 to 23 s | 15 to 23 s |
| Machine weight | 14 t | 12 t |
| Stacker power | 3.0 kW | 3.0 kW |
Take the QST6-15 when the building is compact, the transformer is limited and the target is a steady single-shift output. Take the QST8-15 when you want the higher vibration force for denser blocks, the wider 980 × 860 mm pallet, and headroom to add a second shift. The QST8-15 sits on a 9,800 × 3,600 mm footprint, so check the clear floor space and the crane or forklift access before the foundation is poured.
Both models run the same control philosophy, so an operator trained on one reads the other quickly. If you are comparing what a block moulding machine platform offers in general, the mould interface is the part to understand first, because it sets which products you can add later.
Cement Block Making Machine Capacity and Output
Capacity is not a single number. It is pieces per mould, cycle time, shift length and raw material stability working together, and the block type decides how many pieces fit on the pallet in the first place.
| Model | Standard brick output | Condition |
|---|---|---|
| QST8-15 | Up to 90,000 bricks per 8-hour shift | Standard brick, stable mix, cycle at the fast end |
| QST6-15 | Configured below the QST8-15 | Depends on the mould and the product |
| Hollow blocks | Fewer pieces per shift than solid brick | Lower pieces per pallet and a heavier block |
Three things move the real figure: the moisture in the sand, the accuracy of the batching, and how fast the operator keeps pallets in front of the machine. A host that is starved of pallets or fed an uneven mix never reaches its cycle number, whatever the specification sheet says.
For a planning figure, take the cycle time and the pieces per mould, multiply by the cycles available in a shift, then discount for real stops. If you send your block size and target pieces per shift, the cycle and the model can be matched to it rather than guessed at.
Raw Materials and Mix Design
The machine runs on a dry-cast mix: cement, sand, gravel or crushed stone, and water. Optional additions such as fly ash, slag, stone powder and screened construction waste replace part of the aggregate when the gradation is controlled, and they lower the cement content per block.
- Cement as the binder
- Sand and gravel or crushed stone as the aggregate
- Optional fly ash, slag, gangue or construction waste in place of part of the aggregate
- Water, held tight and consistent, because the dry-cast mix is judged by feel and by the block
The batching tolerance matters more than the headline mix ratio. A batching machine such as the PL series doses fast and then slow to a pre-set aggregate ratio and weighs with three-point induction sensors, so each batch repeats. Uneven dosing shows up as a block that varies in weight from pallet to pallet, which is a sales problem as much as a technical one.
Cure and stacking discipline finish the job. Blocks released wet and stacked too early lose corner strength, so the curing and cubing step deserves the same attention as the host machine.
Main Components and What They Do
A working line is more than the host. The parts below are what a buyer sees when the machine is on site.
- The host machine, where the mix is filled, vibrated and pressed
- A batching machine that doses aggregate by weight to a set ratio
- A mixer, such as the CMP vertical shaft planetary mixer, for a uniform batch
- A pallet magazine fed by an automatic pallet feeding machine, for example the QS-1200, which cycles in about 13 seconds
- A stacker or cuber that lifts the green blocks and builds them into a stack
- A control cabinet and the PLC touch screen that runs the automatic cycle
The pallet feed is the quiet bottleneck on many small plants. The QS-1200 automatic pallet feeding machine keeps the magazine full and runs on 3 kW, small against the host but enough to stop the machine waiting. Ask how many pallets a full cycle needs and add spares, because pallets carry the wear.
What Affects the Price of a Cement Block Making Machine
There is no single price for a cement block making machine, because the line around the host changes the total. Treat the following as the list to compare, quote by quote, rather than a number.
- The host model, QST8-15 or QST6-15, and the pressure and output that come with it
- The number of moulds in the order, which is the single biggest swing after the host
- Whether batching, mixing, pallet feeding and stacking are included or bought later
- The stacker or cuber option, and whether it is manual or fully automatic
- The number of pallets supplied, because they are steel and they ship as weight
- The motor voltage and phase for your site
- Freight, insurance, installation and training
A cheap host with no batching and no spare pallets usually costs more in the first year than a complete line bought once. Ask for the quotation to list every item line by line, then map each line to the factors above. For a fuller breakdown of the cost items, see the block making machine price guide.
Installation, Training and Spare Parts
Installation starts with a level, cured concrete floor and a foundation that matches the machine footprint. Power comes to the control cabinet, and the automatic cycle is commissioned once the mix is set and the first blocks are checked.
- Foundation and floor: levelled and cured before the machine lands
- Commissioning: cycle timing, mould fit and mix tuning checked on your material
- Training: operator training on the touch screen, the mould change and the daily checks
- Spare parts: wear parts list agreed at order, including pallets and mould wear items
Ask for the recommended spare part list with the quotation, not after the first breakdown. Moulds and pallets are the two items you will order again, so their lead time matters as much as their price. If your site is far from a service point, carry the small wear items on site.
Cement Block Making Machines for Syria and the Middle East
Machines for this region are usually specified around three things: voltage, dust and heat. Confirm the site supply, single or three phase and the voltage, so the motors and the control panel are built for it before shipping rather than adapted afterwards.
Dust is constant in a block yard. Filters, sealed panels and a routine cleaning schedule protect the PLC and the sensors, and a covered yard lowers the temperature the machine works in. Local cement and local aggregate differ from plant to plant, so the mix is tuned on your material during commissioning.
For delivery, plan the pallet count and the freight in the same order as the machine, because the pallets travel as weight. To see how the host fits a full plant, review the complete concrete block factory solution or the hollow block production line. Buyers weighing a new machine against a used one should read the block machine for sale guide, and buyers in Syria can check the Syria market page for local conditions.
Get Factory Price. Send your block size, daily output target and site voltage, and CEMBRIQ will come back with a QST8-15 or QST6-15 configuration and a factory price. To move faster, use the request for quotation form and include the first block you plan to sell.